Nuclear plant level gauges For balance-of-plant condensate, feedwater and auxiliary tanks
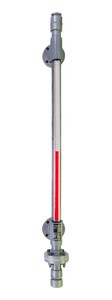
Lamont builds Magnamont™ magnetic level gauges to ASME B31.1 for non-safety-related balance-of-plant service at nuclear generating stations: condensate, feedwater and auxiliary tanks. Stations purchase these gauges to a written specification, with traced materials and a reviewed drawing. Material traceability is maintained throughout manufacturing, and MTRs and hydrostatic test reports are available. The approval drawing is issued after the purchase order for the station’s review. Lamont has supplied gauges for water service at a nuclear generating station in the United States; the station’s engineering group reviewed and signed the approval drawing before fabrication.
- Construction code
- ASME B31.1model code option B1
- Pressure test
- Before shipmenthydrostatic at 1.5 × design where specified
- Material traceability
- MaintainedMTRs available
- Pressure, Magnamont™
- 3,400 psigfull vacuum to 234 bar
Ratings are confirmed at quotation.
Service conditions
Balance-of-plant service
- Purchase specification. The station’s specification sets the piping code, materials, examination and documents. Lamont builds to ASME B31.1 power piping (option B1).
- Traceability. Material traceability is maintained throughout manufacturing, and MTRs are available for the pressure parts.
- Drawing review. The approval drawing is issued after the purchase order, so the station’s engineers can review the design before fabrication.
- Plant piping details. Connections to the plant’s piping specification: socket-weld (Sockolet), Weldolet, flanged or threaded, ½ to 4 in. Special chamber sizes on application review.
- Examination and test. NDE per the governing code where required: visual examination, dye-penetrant examination of fillet welds, and positive material identification (PMI) where specified. Pressure tested before shipment; hydrostatic test at not less than 1.5 × design pressure where specified. Test reports available.
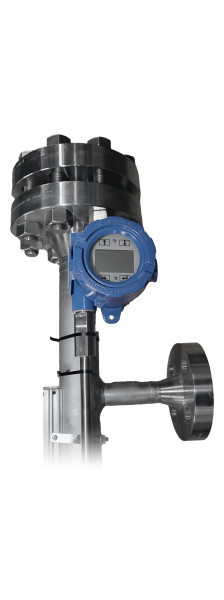
- No additional nozzles. SurePoint™ switches and a LevelSync™ transmitter clamp to the outside of the chamber. They are fitted at the factory or added in the field during an outage.
Recommended build
Typical build for a balance-of-plant tank
| Gauge line | Magnamont™ for condensate, feedwater, auxiliary and water-treatment tanks. Fortimag™ for high-pressure balance-of-plant service |
|---|---|
| Construction code | ASME B31.1 B1 |
| Chamber | Welded SS316, 1.5 in or 2 in; special sizes SP on application review |
| Float | MagnaLine™ titanium TI, weighted for water at operating temperature |
| Connections | Socket-weld (Sockolet SO), Weldolet WO, flanged FL or threaded; ½ to 4 in |
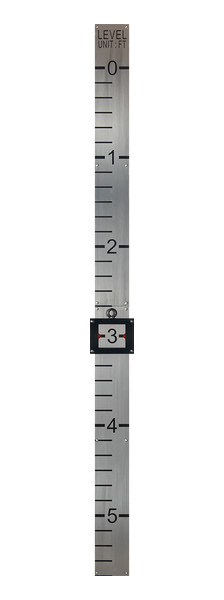
| Indicator and scale | ClearView™ ISFS-300 with an etched aluminum scale; marking to MIL-STD-130N |
| NDE | Per the governing code where required: visual examination, dye-penetrant examination of fillet welds, and positive material identification (PMI) where specified; radiographic (X-ray) or ultrasonic examination of full-penetration butt welds on Fortimag™ |
| Testing | Pressure tested before shipment; hydrostatic test at not less than 1.5 × design pressure where specified. Test reports available |
| Traceability | Maintained throughout manufacturing; MTRs available |
| Drawings | Approval drawing issued after the purchase order, for review before fabrication |
| Further inspection | Available on request |
| Alarms and signal | SurePoint™ latching SPDT switches PLS-1 to PLS-8; LevelSync™ MLT, 4–20 mA with HART® |
Pressure and temperature ratings depend on materials, connections and configuration, and are confirmed at quotation. Quality and document requirements beyond those listed here are reviewed against the purchase specification at quotation. This page covers non-safety-related balance-of-plant service. Nuclear quality-programme requirements, such as 10 CFR 50 Appendix B, ASME NQA-1 or CSA N299, are outside Lamont’s standard scope: state them with the request.
Engineering note
Design conditions and test pressure
Design conditions and float weighting
A balance-of-plant tank often operates well below its design rating. The design conditions set the chamber, flanges and test pressure. The float is weighted for the water at operating conditions.
- Hydrostatic test, where specified: 1.5 × 100 psig = 150 psig (10.3 bar), on the chamber and flanges.
- Flanges: a Class 150 flange in 316 stainless is rated about 225 psig at 250 °F (ASME B16.5, material group 2.2), above the 100 psig design pressure.
- Float: weighted for water at 100 °F, SG 0.99, and rated for the 100 psig design pressure.
Documents and when they are issued
The documents below are available from Lamont, as stated in the specification sheets. Further requirements are reviewed against the purchase specification.
| Document | When |
|---|---|
| Approval drawing | After the purchase order, for review before fabrication |
| Material test reports (MTRs) | Available |
| Hydrostatic test report | Available |
| NDE records | Where the governing code requires examination |
| Further inspection | Available on request |
Applications
Selected projects
Quotation
What to send for a quotation
- The purchase specification, with its piping code, material, examination and document requirements.
- Operating and design pressure and temperature, and the fluid (condensate, feedwater, demineralized or treated water).
- Centre-to-centre distance, connection size and type (socket-weld, Weldolet, flanged or threaded) and the plant’s piping class.
- Tag numbers for each gauge, and the scale units the operators use.
- Level points: alarms and a 4–20 mA signal, if needed, and the area requirements for the instruments.
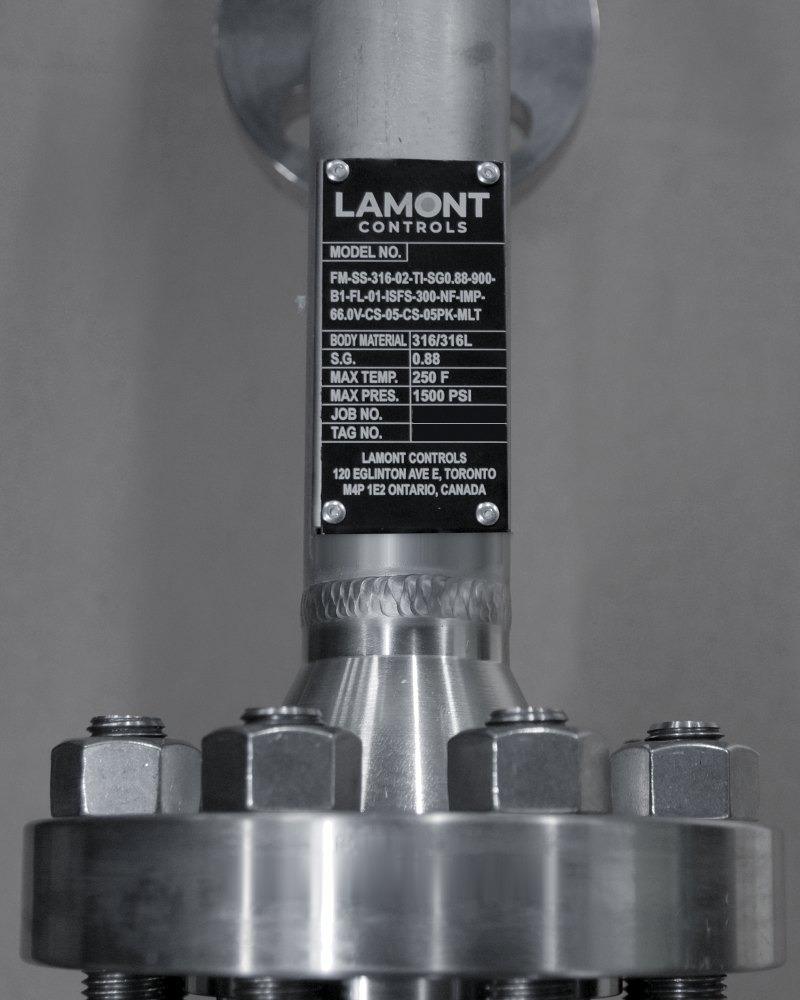
- Replacing an existing gauge: a photo of the nameplate and the existing centre-to-centre. See Retrofits.
Questions
Frequently asked questions
Which construction code applies?
ASME B31.1 power piping (model code option B1). ASME B31.3 and industrial grade construction are also available where the owner’s specification allows.
Which documents are available with the gauge?
MTRs and hydrostatic test reports are available. Material traceability is maintained throughout manufacturing. NDE is performed per the governing code where required. Further inspection is available on request.
Can the station review the drawing before fabrication?
Yes. Lamont issues the approval drawing after the purchase order. On an order for a nuclear generating station, the station’s engineering group reviewed and signed the drawing before fabrication.
Can switches or a transmitter be added during an outage?
Yes. SurePoint™ switches and a LevelSync™ transmitter are externally mounted and magnetically coupled to the same float. They have no wetted parts and need no new vessel nozzle.
Can the plant’s connection and material specification be matched?
Connections are socket-weld, Weldolet, flanged or threaded, ½ to 4 in, with special chamber sizes on application review. The chamber is SS316 as standard. For Hastelloy, Monel K-500, Inconel 625, coated or lined chambers, consult factory.
Applications